A Kanban system is effective when three things hold together: work starts only because downstream demand asks for it, every stage has a hard cap on how much can sit in it, and the team watches how long items take to get through. With those in place, inventory and queues shrink and delivery becomes predictable. Without the caps, Kanban turns into a colourful status display that changes nothing.
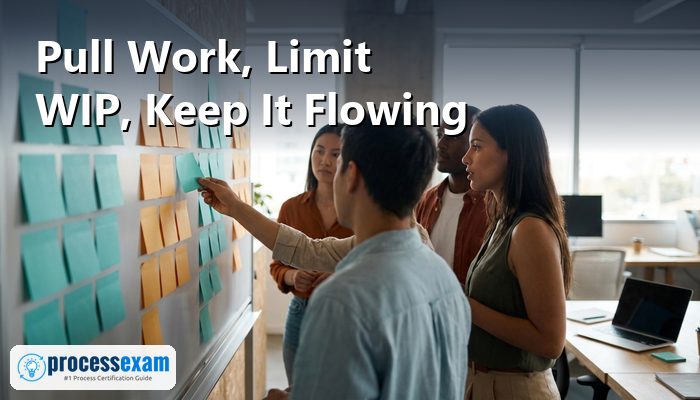
That is the short answer, and it holds for a car plant and for a software team alike. The longer answer explains why the caps matter so much, how to size them, which numbers prove the system is working, and where Kanban is the wrong tool. This page covers the method from its origin in Toyota's machine shop to the boards used by service desks today, and closes with where Kanban appears in the IASSC Lean Six Sigma bodies of knowledge, because it is one of the Lean controls those exams expect you to understand.
What is a Kanban system, and where did the cards come from?
The Japanese word kanban means signboard. In production, a kanban is a signal that authorises work: make this part, or move this container, in this quantity. The signal was originally a card that travelled with a box of parts, and Wikipedia's account of the kanban scheduling system credits Taiichi Ohno, an industrial engineer at Toyota, with developing it to improve manufacturing efficiency. It is also known in the automotive industry as the Toyota nameplate system.
 You have to pass the ICYB exam to receive the certification from IASSC. To increase the effectiveness of your study and make you familiar with the actual exam pattern, we have prepared this sample questions. Our


