How ASQ CQE Certification Shapes the Future of Quality Management?
Updated on 29 October 2026. What’s new: corrected the exam fees to ASQ's current $450 member, $550 non-member and $350 retake prices
The quality standard most employers audit against was revised in September 2026, and the shift in its wording shows where the job is going: less proving that a product was inspected, more showing that its failures were planned for. Quality engineers who can rank risks, read data critically and hold suppliers to account gain from that shift, and those are the strands the ASQ Certified Quality Engineer (CQE) Body of Knowledge is built from.
This article is about the work rather than the exam. It looks at four changes in what quality engineers are asked to do, then matches each change to the part of the CQE syllabus that trains for it. Exam logistics are kept to one short section near the end, because the numbers are already well covered elsewhere.
What has changed in a quality engineer's week?
The clearest recent marker is ISO 9001. The 2026 edition was published on 16 September 2026, and the certification body LRQA reports that organisations certified to the 2015 edition have until 30 September 2029 to transition. LRQA also describes the process approach, the plan-do-check-act cycle and risk-based thinking as still central, with risks and opportunities now treated separately, stronger requirements for planning and communicating changes to the management system, and quality culture written into the leadership requirements. Wikipedia's ISO 9001 entry gives a similar summary and describes the new edition as a measured revision, not a rewrite. Read the standard itself before you quote any clause to an auditor, but the direction of travel is not in doubt.
Strip away the clause numbers and four changes show up in most quality engineering job descriptions, whatever the industry.
From detecting defects to preventing them
A decade ago a good week ended with a clean inspection report. The more common expectation now is a documented answer to a different question: what could go wrong with this design, this process or this supplier, how bad would it be, and what is already in place to stop it? That question sits upstream of the factory floor, in design reviews, process flow diagrams and control plans, so the engineer is in the meeting before any part exists.
From sampled data to a steady stream of data
Sensors, test stations and traceability systems now record far more than a clipboard ever did. The skill that matters is no longer collecting numbers but deciding which numbers deserve trust. A data stream from an uncalibrated gage, or from a process that has quietly changed, is a confident-looking error. Engineers are asked to judge measurement quality, spot when a chart means what it appears to mean, and choose a test that fits the question.
From one factory to a network of suppliers
Many products are now assembled from parts that were designed, made and tested by other companies in other countries. The quality engineer's reach therefore ends at the supplier's gate, not their own. Supplier selection, incoming controls, audits and corrective action requests have become core work instead of a side task.
From passing a test to predicting a lifetime
Customers care less that a unit passed final test and more whether it will still work after three winters or ten thousand cycles. Reliability thinking, which estimates how and when things fail, has moved from specialist teams into the general quality engineering role.
None of these changes replaces the older toolkit of control charts, sampling plans and corrective action. They raise the standard of judgement the toolkit is used with, which is why a knowledge-based credential still has something to say.
Which parts of the CQE Body of Knowledge map to those changes?
The CQE examination is built from a Body of Knowledge in seven areas, which ASQ publishes on its CQE certification page together with the exam format. The areas are not equally relevant to each change, and it helps to see the match before reading the detail. The table below is a reading guide built for this article, not ASQ's own wording: it ties each change to the area that carries most of the matching content.
| Change in the work | Main CQE area | What the syllabus trains you to do |
|---|---|---|
| Preventing rather than detecting | VII. Risk Management, with III. Design | Assess risk with FMEA and risk matrices, then plan controls before launch |
| Trusting data | VI. Quantitative Methods and Tools, with IV. Product and Process Control | Choose the right test or chart, judge capability, and check the measurement system |
| Managing suppliers | I. Management and Leadership, with IV and II | Qualify and audit suppliers, apply sampling plans, run a documented quality system |
| Predicting lifetimes | III. Product, Process, and Service Design | Use reliability models and indices, and carry customer requirements into design |
| Improving what exists | V. Continuous Improvement | Use basic and management tools, lean methods and corrective action to remove root causes |
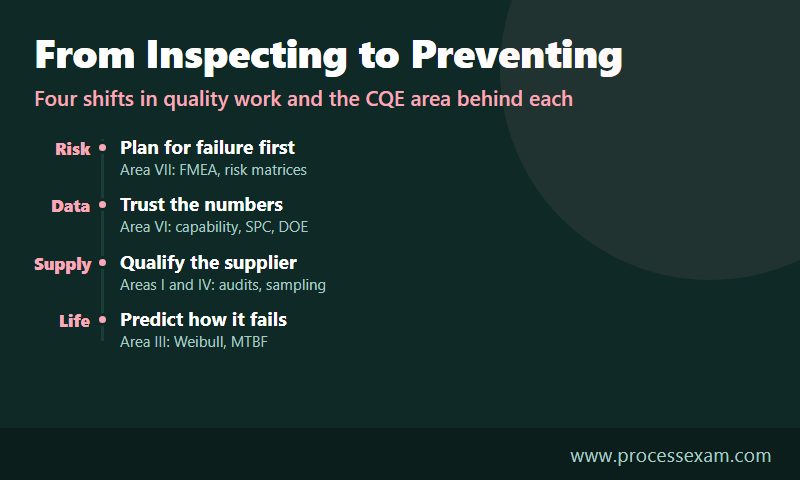
Two observations follow. First, the Body of Knowledge already assigns a full area to risk, and it asks for application and analysis, not memorised definitions. Second, the largest share of exam questions comes from the quantitative area, which matches the shift towards data. The syllabus was not rewritten to follow a trend; it has been this way because quality engineering has always depended on these skills. What has changed is how many employers now say so in their job advertisements.
How does risk-based thinking show up in the work and on the exam?
Risk is the clearest example of a standard and a certification pointing the same way. ISO 9001 has carried risk-based thinking since its 2015 edition, and the exam tests the tools that make it practical: FMEA in its design, process and use forms, risk matrices, risk priority numbers, risk registers, and the treatment of risk through avoidance, reduction, transfer or acceptance.
A worked example: connectors for a battery pack
Imagine a team adding a new supplier of plug-in connectors for a battery pack. A process FMEA lists failure modes for each step. Take one row, an under-crimped terminal. The team scores severity, how serious the effect is for the customer, occurrence, how often the cause is likely to arise, and detection, how likely current controls are to catch it before shipment, each on a scale of 1 to 10. The figures below are invented for illustration.
| Failure mode | Severity | Occurrence | Detection | Risk priority number |
|---|---|---|---|---|
| Under-crimped terminal | 9 | 4 | 5 | 180 |
| Wrong connector variant fitted | 6 | 3 | 2 | 36 |
| Cosmetic scratch on housing | 2 | 5 | 3 | 30 |
The product of the three scores gives the risk priority number, and the crimp row dominates. A useful engineer does not stop at the number, though. The crimp failure has a severity of 9, so it deserves action even if its occurrence falls, and a low-severity row with the same number would not. That judgement is exactly what scenario questions on the exam probe, and it is the reason some industries now rank actions by severity first instead of by the multiplied figure alone.
The corrective step also matters. Raising detection, for example by adding a pull test, is weaker than reducing occurrence by controlling the crimp height, which is weaker still than designing a terminal that cannot be under-crimped. The Body of Knowledge expects you to recognise that ladder from prevention to detection, and the standard's wording on risk-based thinking supports it.
Where risk meets management
Risk work is also a management skill. A risk register is only worth keeping if someone owns each entry, reviews it on a schedule and links it to the quality system. The Management and Leadership and Quality System areas cover that side: planning, ownership, document control and audit follow-up. The new ISO emphasis on planning and communicating change fits here as well, because a changed process is one of the most common sources of fresh risk.
Why do data and reliability skills carry so much weight now?
A shop that records every part can still make poor decisions, because quantity does not fix quality of evidence. The quantitative area of the syllabus is built around that problem. It covers data types, descriptive statistics, probability and distributions, confidence and tolerance intervals, hypothesis tests, analysis of variance, regression, control charts, capability and designed experiments.
Decide what the data can and cannot tell you
Three habits separate an engineer who uses data from one who merely collects it. The first is to ask what the measurement system contributes to the variation before analysing the part-to-part variation; a gage that is too coarse makes every later conclusion unreliable. The second is to match the question to the test: a difference between two suppliers' means calls for a different tool than a comparison of their spread. The third is to look at the chart before running the calculation, since a shift or trend visible by eye usually means that a capability index will mislead.
Reliability in plain terms
Reliability work asks how long, and in what way, something lasts. The Body of Knowledge covers the Weibull distribution, the bathtub curve and indices such as mean time to failure, mean time between failures and mean time to repair. A single Weibull figure shows how useful this is. The shape parameter tells you the pattern of failure: a value below one means failures cluster early, which points at manufacturing or assembly defects; a value near one means failures arrive at random; a value above one means wear-out, which points at material, design or maintenance.
Field return data from a product that shows a shape well above one tells the team to work on durability and maintenance intervals, not on incoming inspection. A shape below one sends effort the other way, towards process controls and burn-in. The engineer who can read that one number saves months of working on the wrong end of the product's life.
Design of experiments belongs in the same toolkit. As products become more complex, trying one factor at a time stops being affordable, and factorial designs let a small number of runs reveal both the main effects and the interactions between factors.
What does supplier quality involve when the supply chain is the factory?
Supplier quality is spread across the Body of Knowledge rather than gathered in one place, and that is itself a clue to how the work really goes. It begins in Management and Leadership with supplier management and customer relations, continues in the Quality System area with audits and document control, and shows up again in Product and Process Control with sampling and material review.
Choose controls to match the supplier's record
Acceptance sampling is the best-known tool. Plans built on the ANSI/ASQ Z1.4 standard apply to attributes, such as conforming or not, while Z1.9 applies to measured variables. Operating characteristic curves show how likely a lot is to be accepted at a given quality level, which makes the risk to both buyer and seller visible. The point to grasp is that a sampling plan is a risk decision, not a guarantee, and for a supplier with a long and stable record the sensible move is often to ask for process capability evidence instead of inspecting every lot.
Audits as evidence, not ritual
A supplier audit is useful when it tests how a process behaves in practice. Auditors look for objective evidence that records match reality, that nonconforming material is segregated and traced, and that corrective actions find root causes. The syllabus covers audit types, roles, planning and reporting, and the follow-up that closes the loop; that follow-up is where many real programmes fall short.
Cost of quality at the supplier gate
Cost of quality connects the technical work to the budget. A defect caught at the supplier's gate costs far less than the same defect found in a customer's hands, which is the argument that wins resources for supplier development. The Body of Knowledge includes the cost categories, so a candidate learns to put the argument in the terms a finance director uses.
How should you read process capability when no process is perfectly stable?
Capability is where statistics meets the customer's specification. Cp compares the width of the specification with the natural spread of the process, and Cpk also penalises a process whose average sits off-centre. Pp and Ppk use the overall spread, including drift over time, so they describe what the customer really received. The CQE syllabus covers all of these, together with Cpm, which accounts for distance from the target.
A short calculation
Suppose a shaft diameter has specification limits of 9.90 and 10.10 millimetres, a process average of 10.02 and a standard deviation of 0.03 (again, invented figures). The specification width is 0.20, and six standard deviations are 0.18, so Cp is 0.20 divided by 0.18, or about 1.11. The average is 0.08 below the upper limit and 0.12 above the lower limit, so the nearer limit governs: 0.08 divided by three standard deviations of 0.09 gives a Cpk of about 0.89.
That is an uncomfortable result. The process has enough spread to fit the specification, since Cp is above one, but it is aimed at the wrong place, so some parts will exceed the upper limit. Re-centring the process on 10.00 would lift Cpk to match Cp without any improvement in variation, which is usually a cheaper fix than reducing spread.
Stability comes first
The most common error in the field is quoting a capability index for a process that is not in statistical control. If the control chart shows a drifting average or points outside the limits, the index describes a moment, not a process. Exam questions test this by giving a chart and a calculation together and asking which conclusion is justified. The honest answer is sometimes that no capability claim can be made yet.
The same logic extends to customers and regulators. As more contracts ask for capability evidence alongside conformance, the engineer who can explain the difference between short-term and long-term indices, and why a number was calculated on a stable process, adds credibility that a bare figure cannot.
What do the CQE facts look like, and where does the credential fit in a career?
The exam facts are short and worth having in one place. The figures below are those used on the ProcessExam exam page; ASQ sets the rules, so check its page before applying.
| Detail | ASQ CQE |
|---|---|
| Exam code | CQE |
| Questions | 175 (160 scored, 15 unscored, on the computer-based exam) |
| Time | Total appointment time - 330 minutes; exam time - 318 minutes |
| Passing score | 550/750 |
| Fee | ASQ members - $450; non-members - $550; retakes - $350 |
| Format | Open book, computer-based at a test centre |
The format rewards preparation of a particular kind. Because the exam is open book, nobody scores on recall alone; the marks go to candidates who know where a formula lives and how to apply it quickly under time pressure. ASQ's calendar currently lists a December 2026 computer-based testing window, with a November application deadline, so check the page for the date that suits you. A set of CQE sample questions shows the scenario style before you commit to a study plan.
What the credential signals to employers
A CQE tells a hiring manager that a candidate has been tested across the whole quality system, not just one tool, and that the experience requirement has been met. For a candidate who works in one narrow area, such as inspection, it signals readiness for broader scope. For a manager building a team, it offers a shared vocabulary: two certified engineers can discuss FMEA, capability or sampling without defining the terms first. ASQ also expects holders to renew the credential through recertification, which ASQ explains on its recertification page, so the credential reflects continued learning rather than a single sitting.
How practice fits into the plan
Studying the Body of Knowledge is the foundation, but candidates who are rusty on calculations tend to benefit from repeated exposure. A CQE practice exam built around the same scenario style makes it easy to see whether you reach for the correct reference quickly enough, and which of the seven areas needs another pass.
What can a certification not do for the future of the role?
A credential is evidence of knowledge at one point in time; it is not a substitute for judgement or for experience with a particular product. Several limits are worth stating plainly.
- It does not teach a specific industry's regulations. The exam deliberately leaves industry-specific standards out, so a medical device engineer still has to learn that sector's rules, and an automotive engineer the customer-specific requirements.
- It does not keep pace with every tool. Software for statistics, quality management and data capture changes often, and the Body of Knowledge describes methods instead of products. Learn the method first, then the tool your employer uses.
- It does not replace communication. Much of the value in the new version of the quality role comes from explaining a risk to a design team or a finding to a supplier in a way that leads to action. The Management and Leadership area touches this, but practice on real projects does the rest.
- It does not remove the need to read the source. Standards are revised, as the 2026 edition of ISO 9001 shows, so an engineer needs the habit of checking the current text of any standard before citing it.
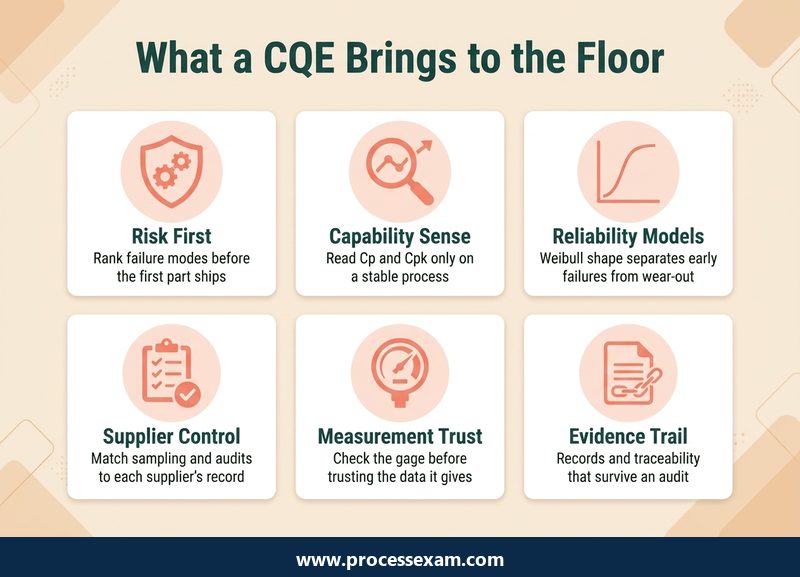
What the CQE does provide is a map. When a manager says the team should be more risk-based, more data-driven or tougher on suppliers, the engineer who has worked through the Body of Knowledge knows which tools those phrases refer to, and what good use of each looks like. That is a narrower claim than shaping the future of the profession, but it is a more honest one, and it is the claim the syllabus supports.
Frequently Asked Questions
What is the ASQ CQE certification?
The Certified Quality Engineer credential is awarded by ASQ to people who show knowledge across a quality system: design, control, statistics, improvement, management and risk. The exam is open book, has 175 questions on the computer-based version, and needs a score of 550 out of 750 to pass.
How much does the ASQ CQE exam cost?
ASQ lists the fee at $450 for members and $550 for non-members, with a retake fee of $350. Fees can change, so confirm them on ASQ's CQE page when you apply, and check whether any local taxes or testing-centre charges apply to your booking.
What is the passing score for the ASQ CQE exam?
The passing score is 550 out of 750. The computer-based exam has 175 questions, of which 160 are scored and 15 are unscored trial questions that cannot be identified. ASQ reports results as a scaled score, not a simple percentage of questions answered correctly.
Is the CQE exam difficult?
Most candidates find the quantitative area the hardest, since it needs statistics, capability and sampling calculations in a limited time. The exam is open book, which helps only if your references are tabbed by topic. Experience in quality engineering usually shortens preparation, and practice questions show weak areas early.
What are the benefits of the ASQ CQE certification?
It shows employers that you have been tested across the whole quality engineering body of knowledge, from risk and design to statistics and audits. It also gives you a common vocabulary with other certified engineers and a structured route to keep learning through ASQ's recertification requirements.
- ASQ Quality Engineer Sample Questions |
- CQE Exam Questions Download |
- CQE Test Questions |
- Quality Engineer PDF |
- ASQ Quality Engineer Book |
- ASQ CQE BOK PDF |
- Quality Engineer Certification Cost |
- Quality Engineer Certification Requirements |
- ASQ Quality Engineer Test Questions |
- CQE Question Bank |
- CQE Body of Knowledge (BOK) |
- Engineering |
- CQE Handbook


